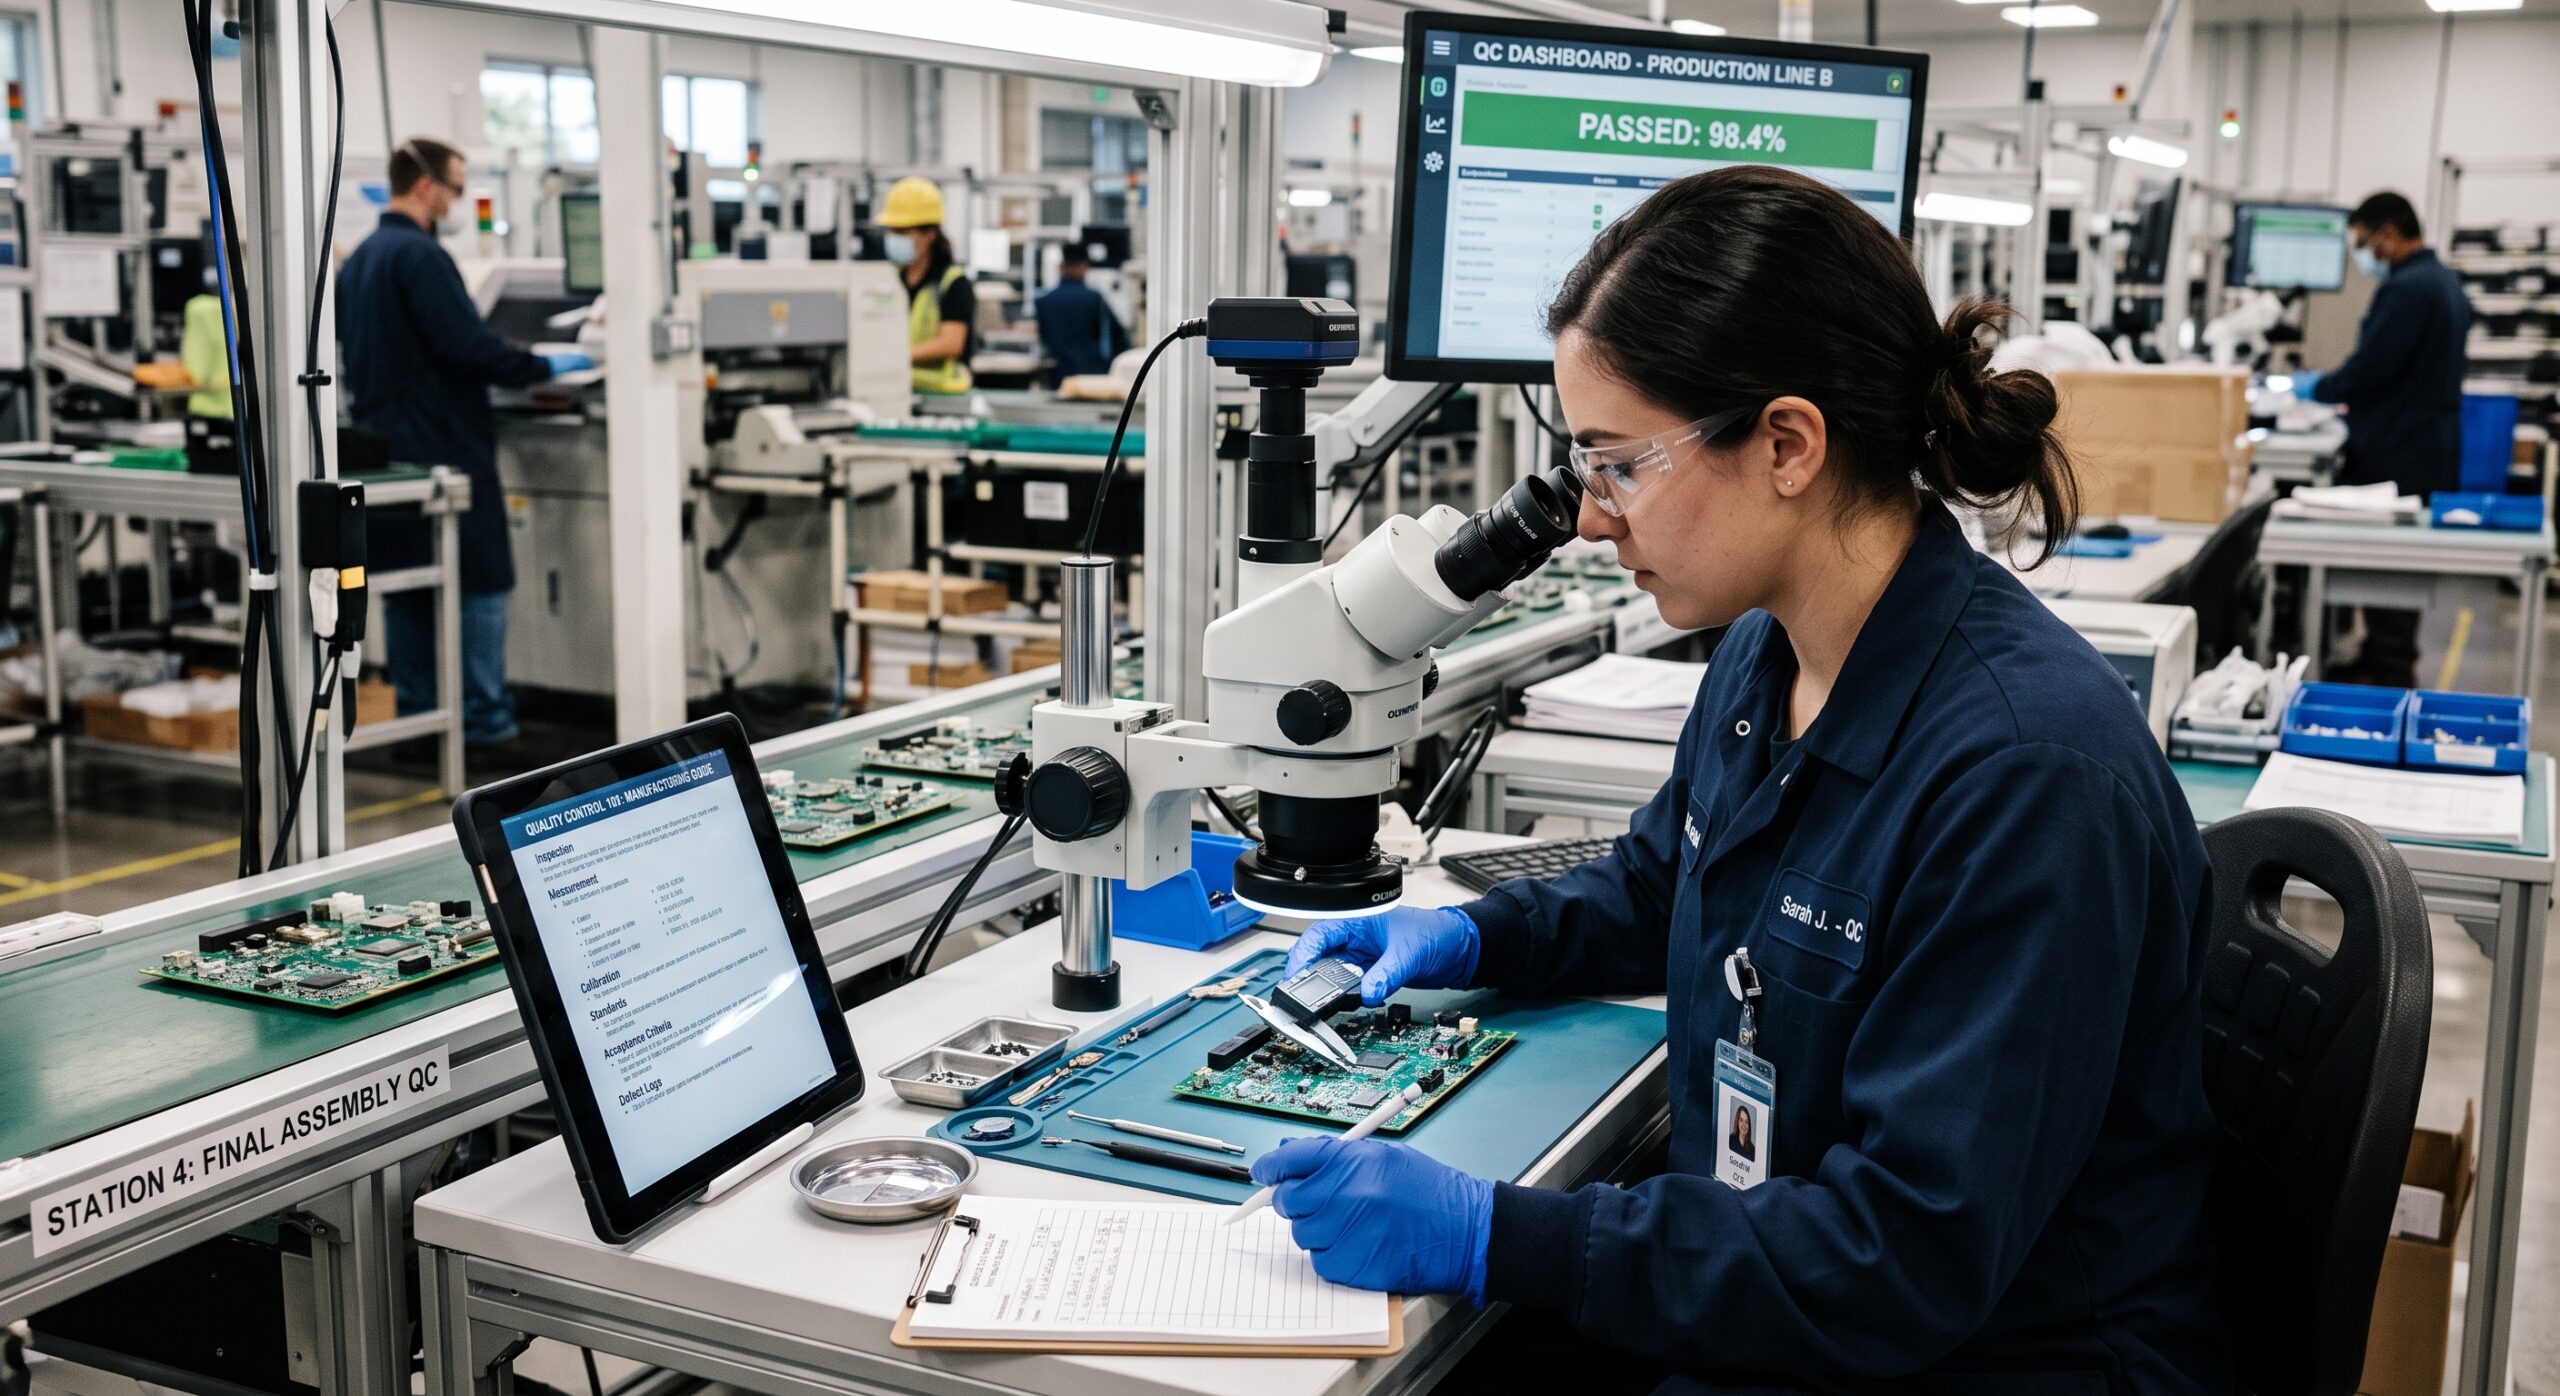
When I first became responsible for quality management manufacturing on a busy production floor, I learned an important lesson: a single careless person or one bad machine setting rarely causes defects. Instead, poorly designed, unmeasured, or uncontrolled processes usually generate them.
For this reason, effective quality management manufacturing programs focus on prevention rather than relying only on final inspection. Indeed, inspection can find a problem, but a reliable quality system prevents the problem from occurring in the first place. Furthermore, ISO describes a quality management system as a collection of processes and procedures that helps a business consistently meet customer, regulatory, and operational requirements. Consequently, it promotes a continuous cycle of planning, doing, checking, and improving.
For new factory managers, this distinction is critical. Ultimately, your objective goes beyond identifying defective products at the end of the line. Rather, your objective centers on building a production system in which workers find it difficult to create defects, easy to detect them, and unlikely to repeat them.
Therefore, managers should treat zero-defect manufacturing as a direction and operating discipline, not as an unrealistic promise that variation will never occur. In real factories, raw materials, equipment, people, environmental conditions, and product designs all introduce variation. As a result, the practical goal focuses on preventing defective products from reaching the customer while continually reducing the root causes of defects inside the plant. In fact, research on quality management manufacturing describes this approach through four connected activities: detect, predict, repair, and prevent.
What Quality Control Means in Quality Management Manufacturing
Quality control evaluates whether products and processes meet defined requirements. Specifically, it includes inspecting, measuring, testing, sampling, monitoring processes, and controlling nonconforming material.
On the other hand, quality assurance takes a broader scope. It examines whether the process itself can produce acceptable results consistently. In simple terms, quality control asks, “Is this product acceptable?” Meanwhile, quality assurance asks, “What must we do so we produce acceptable products every time?”
Undoubtedly, both functions matter. A factory that only inspects finished goods may discover problems too late, after wasting materials, labor, and machine time. Conversely, a factory that only documents procedures without checking actual output may create an impressive system that fails to reflect reality.
Therefore, strong quality management manufacturing systems connect both sides. First, leadership clearly defines requirements and standardizes processes. Next, supervisors train operators so measurements remain trustworthy. Furthermore, teams contain defects quickly and thoroughly investigate their root causes. Finally, managers verify corrective actions so that improvements permanently integrate into the standard process.
For managers, this means the inspection department cannot own quality alone. Instead, production, maintenance, engineering, purchasing, warehousing, and leadership all drive the final result.
Start With Clear Requirements
Naturally, a factory cannot control quality if employees do not know what “good” looks like. Therefore, before changing inspection methods or purchasing software, review the requirements for each product and process within your quality management manufacturing framework.
Requirements may stem from customer drawings, specifications, contracts, industry standards, safety regulations, internal engineering documents, or approved samples. Above all, make sure your team keeps the current version available at the point of use. Indeed, an outdated drawing or unclear work instruction can create more defects than an inexperienced operator.
For every important product characteristic, define the target value, acceptable tolerance, measurement method, and required equipment. Additionally, establish the inspection frequency, name the person responsible for recording results, and outline the exact response operators must execute when results fall outside limits.
Consequently, avoid vague instructions such as “check appearance” or “assemble correctly.” Instead, explain specifically what the operator should look for, using photographs, samples, diagrams, or simple acceptance criteria where appropriate.
A practical example involves torque control. For instance, instead of instructing an operator to “tighten the fastener securely,” specify the exact torque range, tool, calibration interval, verification method, and action to take if the result falls out of range. Ultimately, clear requirements reduce arguments, rework, and inconsistent decisions between shifts.
Use Process Mapping in Quality Management Manufacturing
One of the fastest ways for a new factory manager to understand quality risk involves mapping the process from incoming material to shipment.
To do this effectively, walk the process in sequence. First, record each operation, inspection point, handoff, storage location, machine, tool, and decision. Next, speak directly with the people who perform the work. As a result of this step, you may discover that actual floor practices differ significantly from the documented process.
At each step, ask five key questions:
- What enters this operation?
- What happens to the material?
- What can go wrong?
- How would we know?
- What prevents the problem from continuing?
Consequently, this exercise often reveals hidden risks, such as mixed batches, unclear status labels, missing inspection records, duplicate data entry, or measurements that operators take after a defect has already spread through a large production lot.
Furthermore, process mapping helps managers place controls where they deliver the greatest value. For example, a dimensional check immediately after machining yields better results than discovering the same issue during final assembly. Thus, early detection prevents defective work from moving downstream and significantly reduces the cost of correction.
Standardize the Work
Standardized work stands out as one of the most effective quality control techniques in quality management manufacturing because it systematically reduces unnecessary variation. However, a good standard does not merely describe the task. In addition, it explains the correct sequence, important settings, quality checkpoints, safety considerations, and reaction plan.
Specifically, write standards in language operators understand and place them directly at the workstation. Illustrate them when tasks involve complex or visual elements, review them after engineering or process changes, confirm them through practical training, and routinely audit them during normal production.
At the same time, do not equate a signed training form with genuine competence. An employee may attend training and still fail to perform the task correctly. Therefore, use demonstrations, first-piece verification, skill checklists, and supervised practice to confirm real understanding.
Moreover, standards must reflect actual working conditions. If operators routinely bypass a step because it proves impractical, do not simply blame them. Instead, investigate why they bypass the step. For example, an unclear instruction, an unavailable tool, or aggressive production targets might unintentionally encourage shortcuts. Simply put, an unworkable standard will not control quality.
Build Quality Into the Process
Final inspection serves a purpose, but teams should not rely on it as the primary defense against defects. Instead, robust quality management manufacturing builds quality directly into the process through mistake-proofing, automatic checks, interlocks, fixtures, sensors, and clear visual controls.
Mistake-proofing, often called poka-yoke, designs equipment or methods so that the system either completely prevents an error or immediately identifies it. Examples include a fixture that accepts a component in only one orientation, a connector that prevents incorrect insertion, a sensor that confirms the presence of a required part, a software check that blocks the release of an incomplete job, or a torque tool that locks the process when results fall outside limits.
Ultimately, these controls offer far more dependability than relying on people to remember every detail under pressure. Because human attention fluctuates with fatigue, workload, noise, and interruptions, a well-designed process reduces the manual decisions operators must make. Furthermore, when engineers cannot implement mistake-proofing, apply layered checks instead. For example, an operator can verify the setup, a machine can monitor a critical parameter, and a supervisor can complete a first-piece review after a changeover.
Apply Statistical Process Control
Statistical process control (SPC) helps managers distinguish normal process variation from unusual variation that requires investigation. Specifically, a control chart plots measurements over time against calculated control limits. As a result, it reveals trends, shifts, cycles, or unusual points before a process produces consistently defective products.
Generally, SPC delivers the best results when engineers apply it to characteristics that directly impact product performance and suffer from process variation. Key examples include dimensions, temperature, pressure, fill volume, strength, electrical resistance, or assembly torque.
However, do not place every available measurement on a control chart. Instead, start with the characteristics that drive safety, function, customer satisfaction, or cost.
A basic SPC program requires a defined sampling method, a consistent measurement procedure, reliable and calibrated equipment, clear control limits, rules for recognizing abnormal patterns, and a documented response plan.
Crucially, control limits differ from specification limits. On the one hand, specification limits describe what the customer or engineer will accept. On the other hand, control limits describe the natural behavior of the process based on data. Therefore, a process can run stably while consistently producing material outside specification. Conversely, it can meet specifications today while exhibiting an unstable trend that will generate defects tomorrow.
Ultimately, SPC must trigger action, not sit as decoration on a wall. Thus, when a chart signals unusual variation, stop immediately and investigate the underlying process conditions.
Verify Measurement Systems
Because poor measurements drive poor decisions, you must confirm that your measurement system performs properly before reacting to process data.
Specifically, measurement system checks include calibration, repeatability, reproducibility, bias, stability, and resolution. However, an instrument that passes technical calibration may still fail to measure a specific tolerance accurately. In addition, a gauge may produce varying results depending on who uses it or how the operator positions the part.
To prevent this, ask if the instrument offers enough accuracy for the tolerance and whether it provides adequate resolution. Confirm that managers properly train operators in its use, clear instructions define the measurement method, and workers position the part consistently. Finally, evaluate whether environmental factors such as temperature, lighting, vibration, or cleanliness alter the results.
Consequently, if two inspectors measure the same part and reach different conclusions, the problem may not reside in the part itself. Rather, the gauge, method, training, or acceptance criteria might cause the discrepancy. Therefore, conduct measurement system analysis before launching SPC, approving a new process, or rejecting a supplier shipment.
Control Incoming Materials in Quality Management Manufacturing
Many factory defects originate before production even starts. For example, suppliers may ship material with the wrong grade, incorrect labels, damage, contamination, off-tolerance dimensions, or incomplete documentation.
For this reason, create an incoming quality process based on supplier risk within your quality management manufacturing strategy. Naturally, not every material requires the same level of inspection. For instance, critical components require certificates, testing, traceability, or detailed sampling. Conversely, workers can verify low-risk materials simply through identification and packaging checks.
Important controls include approved supplier lists, clear purchase-order specifications, lot identification, material certificates, receiving inspection plans, quarantine procedures for unapproved material, supplier performance reviews, and visible status labels.
In addition, never store rejected material near approved stock. Instead, rely on physical separation and visible status labels, which provide simple yet powerful control.
Finally, manage supplier quality through ongoing communication and joint improvement, rather than relying solely on rejection. When a supplier problem occurs, provide clear evidence, request a thorough root-cause analysis, and verify that the corrective action actually fixes the issue.
Use Root-Cause Analysis
A corrective action that only fixes an immediate symptom rarely prevents recurrence. Therefore, effective root-cause analysis asks why the defect occurred and why the existing system failed to prevent or detect it.
Useful methods include the 5 Whys, cause-and-effect diagrams (Ishikawa/Fishbone), fault-tree analysis, process reviews, and data stratification. Naturally, match the chosen method to the seriousness and complexity of the problem.
For example, the 5 Whys offers great value when teams use it carefully. However, do not stop at statements such as “the operator made a mistake.” Instead, continue asking why the system allowed the mistake in the first place. Perhaps an unclear work instruction, a visually confusing part, out-of-date training, or an aggressive production schedule encouraged an unsafe shortcut.
Accordingly, a complete investigation examines people, equipment, materials, methods, measurement, environment, and management systems.
Furthermore, always separate containment from corrective action. On the one hand, containment protects the customer immediately by stopping shipments, sorting material, or increasing inspection. On the other hand, corrective action modifies the underlying system so the problem rarely returns. Finally, close the loop by checking effectiveness after implementation. If the defect reappears, the team failed to address the true root cause.
Track the Right Metrics for Quality Management Manufacturing
Because metrics heavily drive behavior, focusing solely on production volume signals to employees that speed matters more than quality. Therefore, a balanced scorecard for quality management manufacturing includes measures that reflect both overall output and underlying process health.
Useful measures include first-pass yield, scrap rate, rework hours, defects per unit, customer complaints, warranty returns, supplier defects, on-time corrective-action closure, process capability, and the cost of poor quality.
Importantly, do not use metrics to punish individual operators for every defect. Instead, use them to identify weak processes and prioritize system improvements. For instance, a sudden spike in rework often points directly to a tooling issue, an unclear setup procedure, a material change, or a maintenance failure.
In addition, review metrics at the right frequency. Operators need immediate, real-time feedback on process conditions. Meanwhile, supervisors should review trends daily, and factory leadership should examine recurring losses, customer impact, and improvement progress weekly or monthly. Ultimately, the most valuable metric tracks the speed and effectiveness of your team’s response rather than the raw count of defects.
Create a Practical Manager Routine
New factory managers can establish control without attempting to overhaul everything at once. Instead, a disciplined, phased routine reveals problems early.
First Five Working Days
During your first five working days, walk every major process, review the top five defect categories, and observe one complete changeover. Additionally, check the status of gauges and test equipment, speak with operators across all shifts, review open customer complaints, and confirm that staff strictly control rejected material.
First Month
During your first month, select three critical product characteristics, create or update process control plans, and review work instructions directly at workstations. You should also establish a daily quality meeting, assign owners to recurring problems, verify supplier controls, and audit one process each week.
First Quarter
During your first quarter, complete measurement system reviews for critical gauges, launch SPC on suitable characteristics, and implement at least one mistake-proofing improvement. Finally, review corrective actions for effectiveness, train supervisors in basic root-cause analysis, and publish quality priorities and results transparently.
Ultimately, progress stems from consistent follow-through. A single massive initiative will not make a factory reliable. Rather, hundreds of small, correct decisions executed every day build reliability over time.
The Role of Culture in Quality Management Manufacturing
Slogans alone cannot build a zero-defect mindset. Instead, workers must genuinely believe that reporting a problem brings constructive support rather than automatic blame.
Therefore, empower employees to stop the process whenever they discover a serious issue. In addition, recognize early detection, make abnormal conditions visible, and treat near misses as valuable opportunities to improve. Conversely, when management ignores defects simply to hit shipment targets, employees quickly learn that leadership views quality as optional.
As a QA Manager, I would rather receive ten honest defect reports during a shift than discover one hidden problem after a customer files a complaint. After all, early information gives the team a real chance to contain the issue, learn from it, and improve the system.
Finally, a strong culture in quality management manufacturing actively involves operators in process improvement. Because operators interact with equipment continuously, they know which steps feel awkward, prove unreliable, or cause performance issues. Consequently, their hands-on experience leads to practical improvements that managers easily overlook in conference rooms.
Frequently Asked Questions
What is quality management manufacturing?
Quality management manufacturing represents the coordinated system of processes, people, controls, measurements, and improvement activities that ensures manufactured products meet customer, regulatory, and internal requirements. Specifically, it encompasses both quality assurance and quality control.
Is zero-defect manufacturing realistic?
Complex production environments struggle to achieve absolute zero defects because systems cannot eliminate variation completely. However, a realistic zero-defect strategy focuses on preventing defective products from reaching customers, detecting problems early, and systematically reducing the causes of defects over time.
What should a new factory manager inspect first?
Start by examining customer complaints, top recurring defects, critical product characteristics, measurement equipment, incoming material controls, and processes with high scrap or rework. In addition, walk the production line to compare written procedures against actual floor practices.
How often should workers inspect finished products?
Product risk, process capability, customer requirements, regulatory expectations, and the reliability of in-process controls dictate the correct inspection frequency. For instance, stable and capable processes require less final inspection, whereas high-risk or unstable processes require much tighter controls.
What are the most important tools in quality management manufacturing?
Begin with practical, core tools: check sheets, process maps, control plans, control charts, Pareto analysis, cause-and-effect diagrams, 5-Why analysis, calibration routines, audits, and mistake-proofing. Ultimately, the best tool simply helps your team understand and resolve the specific problem at hand.
What is the difference between quality assurance and quality control?
Quality control evaluates products and process outputs to determine whether they meet requirements. On the other hand, quality assurance focuses on the underlying systems, procedures, and overall methods that produce those results consistently. A dependable operation requires both.
How can a factory reduce rework quickly?
First, contain the immediate issue. Then, identify where the defect originated, verify the measurement method, review recent operational changes, separate affected material, and implement a targeted corrective action. Above all, avoid adding more final inspection without investigating the root cause.
Should inspectors verify 100 percent of every product?
Not necessarily. While critical characteristics or high-risk products warrant 100% inspection, this approach costs significant money and can still miss defects due to inspector fatigue. Consequently, in-line controls, automated detection, capable processes, and mistake-proofing often deliver far better results.
Reference Section
- American Society for Quality (ASQ). What is a Quality Management System (QMS)? — A comprehensive guide on quality management systems, core principles, frameworks, and practical implementation loops.
- American Society for Quality (ASQ). Learn About Quality: Definitions & Tools — An authoritative glossary and resource repository covering standard quality control tools, root-cause methods, and statistical controls.
- Coherent Market Insights. How ISO 9001 Drives Continuous Improvement in Quality Management Practices — An industry analysis explaining how risk-based thinking and ISO standards build sustainable continuous improvement cultures.
- Frontiers in Manufacturing Technology. Zero-Defect Manufacturing Terminology Standardization: Definition, Improvement, and Harmonization — Open-access research by Psarommatis et al. defining zero-defect manufacturing strategies, Industry 4.0 integration, and defect reduction methodologies.
- Emerald Insight. An Integrated Approach of Zero Defect Manufacturing to Avoid Defect Occurrence in Production — Peer-reviewed study detailing the detect, predict, repair, and prevent frameworks within modern quality management manufacturing systems.
The central lesson remains straightforward: workers do not add quality to a product at the end of production. Rather, clear requirements, capable processes, reliable measurements, trained people, rapid response, and continual improvement create quality throughout the build. For a new factory manager, mastering quality management manufacturing represents the clearest path toward fewer defects, lower costs, stronger customer trust, and a far more dependable operation.