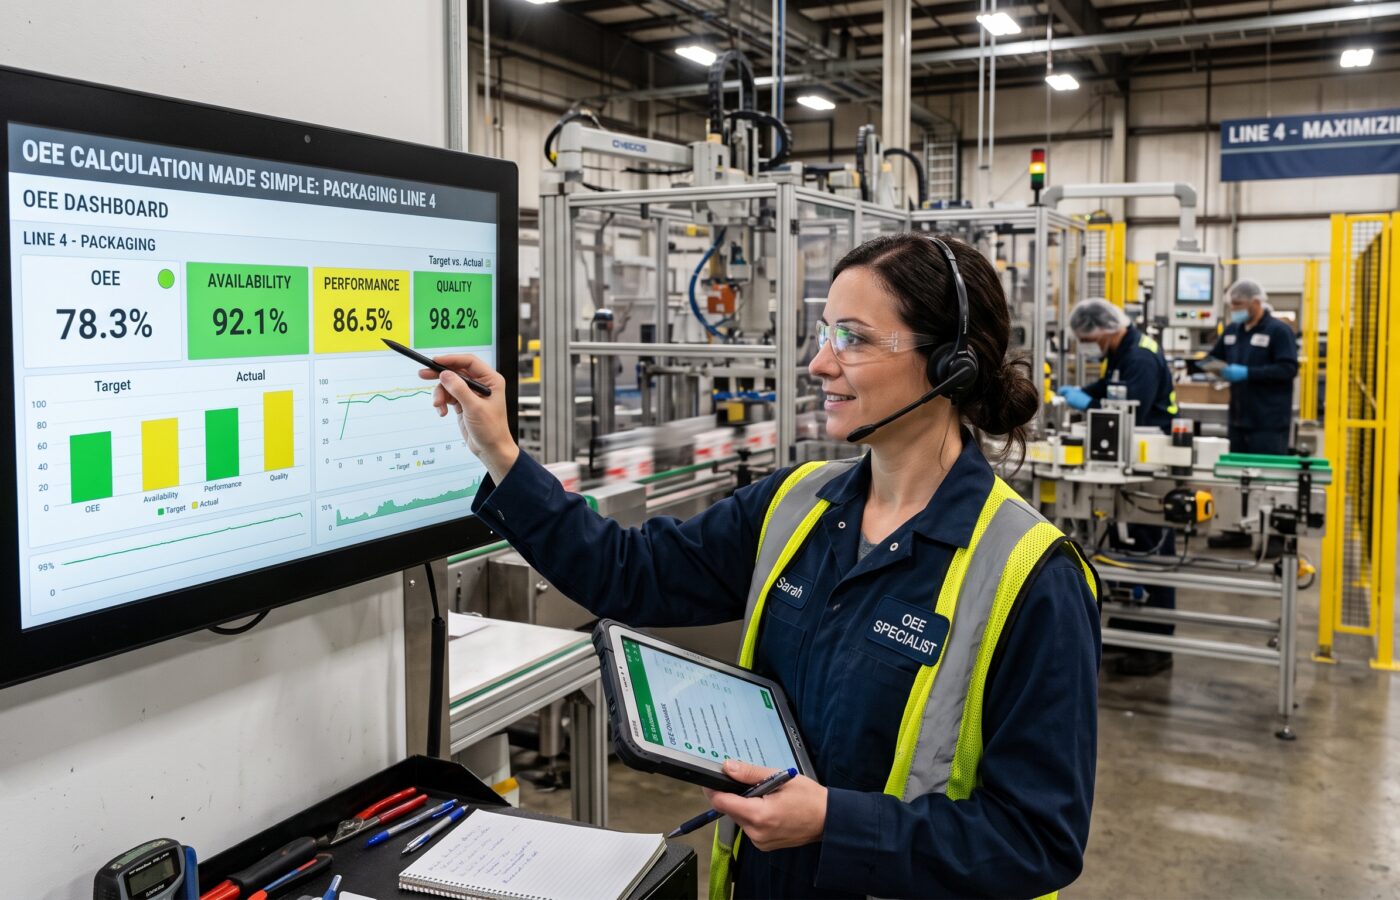
OEE Calculation Made Simple: How to Measure and Improve Equipment Effectiveness

The first OEE calculation I ever presented to a plant leadership team made the room go quiet for all the wrong reasons. We had just finished a three week study on our main packaging line, and the number on the screen was 52 percent. Immediately, the production manager looked at me and said, “That can’t be right. That line runs all day.”
To be fair, he was not wrong about that. The line did run all day. However, it did not run well all day. It stopped for a few minutes here and there, it ran slower than it was designed to on certain products, and it made a steady trickle of rejects that nobody counted because they went straight into a bin by the case packer. On their own, none of those losses felt big. Stacked together, though, they swallowed almost half the line’s real capacity.
OEE Is a Flashlight, Not a Score
That meeting taught me something I still repeat to every new supervisor I train. OEE is not a score to make people look good or bad. Instead, it is a flashlight. In other words, the value of an OEE calculation is not the number itself, but what the number forces you to go look at.
In this article, I want to walk you through OEE calculation the way I teach it on the shop floor. That means no jargon for the sake of it, one clear worked example, the traps I have watched good teams fall into, and finally the improvement approach that has actually moved the needle in the plants I have worked in.
What OEE Actually Measures
At its core, every OEE calculation answers one simple question: of the time you planned to make product on a machine, how much of it produced good parts at the ideal speed?
That is it. Everything else, in fact, is detail.
To make that question useful, OEE breaks it into three parts, and each part isolates one type of loss:
- Availability asks whether the machine was running when it was supposed to be running. As a result, it captures stops, both planned stops like changeovers and unplanned stops like breakdowns.
- Performance asks whether the machine ran as fast as it should when it was running. Therefore, it captures slow cycles and small stops that nobody logged.
- Quality asks whether what came off the machine was good the first time. Consequently, it captures scrap and rework.
When you multiply the three together, you get OEE. A score of 100 percent means the machine made only good parts, at maximum speed, with no interruptions. Of course, nobody gets there, and nobody should expect to. Still, the gap between where you are and 100 percent is your hidden factory, the capacity you already paid for and are not getting.
Where OEE Came From
The concept came out of Total Productive Maintenance in Japan. Specifically, Seiichi Nakajima introduced TPM, OEE and the Six Big Losses in the early 1970s at the Japanese Institute of Plant Maintenance, and later published the benchmarks in his book Introduction to TPM. Remarkably, fifty years later, the core logic has not needed to change, which tells you something about how useful it is.
The OEE Calculation, Step by Step
Before you touch a formula, you need four inputs. If you get these wrong, then your OEE calculation will be wrong no matter how carefully you multiply.
- Planned Production Time. This is the time the machine was scheduled to produce. First, start with the shift length, and then subtract planned breaks, lunches, and time the line was simply not scheduled.
- Run Time. This equals Planned Production Time minus all stop time during that window, whether the stop was a breakdown, a changeover, or waiting on material.
- Ideal Cycle Time. This is the fastest theoretical time to produce one part. Admittedly, it is the number people argue about most, so I will come back to it later.
- Total Count and Good Count. These are every part the machine made, and the ones that passed first time with no rework.
The Four Core Formulas
With those four inputs in hand, the formulas are straightforward.
Availability = Run Time ÷ Planned Production Time
Performance = (Ideal Cycle Time × Total Count) ÷ Run Time
Quality = Good Count ÷ Total Count
OEE = Availability × Performance × Quality
The Shortcut Method
In addition, there is a shortcut. If you substitute the three factor formulas into the OEE equation and simplify, you end up with OEE equal to Good Count multiplied by Ideal Cycle Time, divided by Planned Production Time. Personally, I use the shortcut as a sanity check. For instance, if the long method and the short method do not match, then someone made a data entry error.
A Worked Example From a Real Shift
Now let me put numbers to a full OEE calculation using a shift that looks a lot like ones I have analyzed many times. Picture a filling line running a single eight hour shift.
Steps 1 to 3: Time and Availability
Step 1: Planned Production Time. The shift is 480 minutes. Within it, there are two 15 minute breaks, so 30 minutes of planned downtime. As a result, that leaves 450 minutes of Planned Production Time.
Step 2: Run Time. During the shift, the line had one jam on the capper that took 35 minutes to clear. In addition, a product changeover took 25 minutes. Altogether, that is 60 minutes of stop time. Therefore, Run Time = 450 minus 60 = 390 minutes.
Step 3: Availability. Availability = 390 ÷ 450 = 86.7 percent.
Steps 4 and 5: Performance and Quality
Step 4: Performance. The line’s ideal cycle time is 1 second per bottle, or 60 bottles per minute. Meanwhile, the counter at the end of the shift shows 19,500 bottles produced.
So, the ideal time to make those bottles = 19,500 × 1 second = 19,500 seconds.
Similarly, Run Time in seconds = 390 × 60 = 23,400 seconds.
Consequently, Performance = 19,500 ÷ 23,400 = 83.3 percent.
Step 5: Quality. Of those 19,500 bottles, 585 were rejected for underfill or bad caps.
Therefore, Good Count = 19,500 minus 585 = 18,915.
Finally, Quality = 18,915 ÷ 19,500 = 97.0 percent.
Step 6: The Final OEE Score
OEE = 0.867 × 0.833 × 0.970 = 70.1 percent.
Next comes the sanity check with the shortcut: 18,915 good bottles × 1 second = 18,915 seconds of fully productive time. Then, divide by 27,000 seconds of Planned Production Time, and you get 70.1 percent. Same answer. Good.
What the Numbers Are Really Telling You
Here is the part that matters most. Of 450 planned minutes, only about 315 minutes were fully productive. In other words, roughly 135 minutes, more than two hours, disappeared into stops, slow running, and rejects. That is the conversation you want to have with your team, rather than simply “we got 70.”
Notice something else, too. None of the three factors looks terrible on its own. 87, 83, 97. In fact, a supervisor looking at any one of those would probably shrug. Instead, the multiplication is what exposes the real picture, and that is exactly why OEE works. As eMaint points out, strong scores in each individual area can still multiply into an OEE that is well below where you want it.
The Six Big Losses: Where Your Minutes Go
Once you have your OEE calculation, the next question is always “why.” That is precisely where the Six Big Losses come in. Each loss sits under one of the three factors.
Availability Losses
- Equipment failure. This covers breakdowns, tooling failures, and unplanned maintenance, such as the capper jam in our example.
- Setup and adjustments. This includes changeovers, warmups, material swaps, and the time between the last good part of one run and the first good part of the next.
Performance Losses
- Small stops. These are short interruptions, usually under a few minutes, that operators clear without calling anyone. Typical examples include blocked sensors, misfeeds, or a bottle down on the conveyor.
- Reduced speed. This means running below the ideal rate, often because someone slowed the machine down years ago to fix a problem and nobody ever turned it back up.
Quality Losses
- Production rejects. These are scrap and rework during steady state running.
- Startup rejects. Similarly, this is scrap made while the line comes up to temperature, pressure, or registration after a changeover or restart.
Why the Quiet Losses Matter Most
In my experience, most teams instinctively go after breakdowns first because they are loud and visible. After all, somebody gets called, a work order gets written, and the plant manager hears about it. By contrast, small stops and reduced speed are quiet. They hide inside the Performance number, and moreover, they are frequently bigger. For example, Godlan’s review of published studies found that performance losses often exceeded availability losses, with reduced speed ranking as the top loss on more lines than any other category.
I once spent a week standing next to a labeling machine with a stopwatch and a clipboard. Beforehand, the operators told me it “barely ever stops.” Yet I logged 140 stops in five shifts, almost all under 90 seconds. To be clear, nobody was lying. Those stops simply did not register as stops to the people living with them. For that reason, I push hard for automated counting wherever the budget allows. Indeed, iFactory notes that the gap between reported OEE and actual OEE is typically 8 to 15 points in plants that rely on manual reporting. That matches what I have seen almost exactly.
What Is a Good OEE Score?
Once the OEE calculation is done, everyone wants a benchmark, so here is the honest answer.
The number you will hear most is 85 percent as “world class.” Specifically, that figure comes from TPM literature and is usually broken down as roughly 90 percent Availability, 95 percent Performance, and 99 percent Quality, which multiply to about 84.6 percent.
However, here is the reality check. Vorne, the company behind OEE.com, says most manufacturers still sit closer to 60 percent, and they see more plants below 45 percent than above 85.
A Practical Scoring Guide
As a rough guide, I share these bands with teams:
- Below 40 percent: something fundamental is broken. So, start with data accuracy, then chase the biggest availability loss.
- 40 to 60 percent: typical for a plant just starting to measure. Fortunately, there is lots of low hanging fruit.
- 60 to 85 percent: solid. At this stage, however, improvement takes discipline and structured problem solving.
- 85 percent and above: excellent for discrete manufacturing. Therefore, protect it.
How to Set a Realistic Target
My strong advice is this: do not set 85 percent as a target on day one. Otherwise, it demoralizes the team and invites people to game the inputs. Instead, set a target that is a meaningful step from your own baseline, hit it, and then raise it. Ultimately, the trend line matters far more than the absolute number. For example, a line that moves from 48 to 61 percent in six months has done something remarkable, even if it is still “below average” on paper.
Also, be careful comparing OEE between lines or between plants. A high speed bottling line, an automotive assembly line, and a job shop CNC cell running dozens of different parts a week live in completely different worlds. As a result, it is better to compare a line to itself over time.
Common OEE Calculation Mistakes I See Over and Over
I have audited OEE reporting in a lot of facilities, and the same mistakes show up nearly everywhere. So, if your numbers look suspiciously good, check these first.
Mistakes With Cycle Time and Changeovers
1. Using the wrong ideal cycle time. This is the big one. Often, teams use the “standard” rate, meaning the rate they usually hit, instead of the true design or demonstrated maximum rate. Consequently, that quietly inflates Performance, sometimes by 15 or 20 points. In fact, if your Performance ever comes out above 100 percent, your ideal cycle time is wrong. Full stop. OEE.com is clear that Performance should never be greater than 100 percent. Therefore, use the nameplate speed or the best sustained rate you have ever demonstrated, whichever is faster.
2. Leaving changeovers out of the calculation. Some plants treat changeovers as “planned” and subtract them from Planned Production Time. Unfortunately, that hides one of the Six Big Losses and removes any incentive to shorten them. Changeovers, therefore, belong in Availability. If you want to track schedule driven time separately, then that is what TEEP and utilization metrics are for.
Mistakes With Counting and Stops
3. Counting reworked parts as good. OEE Quality should reflect first pass yield. After all, a part that had to be reworked was not good the first time, and it consumed capacity twice. For that reason, count it as a loss. This matters even more in automotive parts work, where first pass yield is tracked closely.
4. Ignoring small stops. If you only log stops over five minutes, those short interruptions fall into Performance as unexplained loss. Admittedly, that is not wrong mathematically. Nevertheless, you lose the ability to see what caused them. So, set a short stop threshold, somewhere around two minutes, and categorize everything above it.
Mistakes With Reporting and Culture
5. Averaging OEE percentages across lines. For example, if Line A ran 20 hours at 80 percent and Line B ran 4 hours at 40 percent, the plant OEE is not 60 percent. Instead, weight it by time, or better yet, sum up the fully productive time and divide by total planned time.
6. Treating OEE as a performance review tool. The moment OEE becomes a stick to beat operators with, the data starts getting cleaned up before it reaches you. As a result, stops get relabeled as “planned,” and scrap goes uncounted. In short, OEE works when it belongs to the team running the line.
How to Actually Improve OEE
Calculating OEE is the easy part. Moving it, on the other hand, is where continuous improvement and lean principles earn their keep. The following is the approach I use, and it has worked in food, packaging, metal stamping, and plastics.
Step 1: Get Honest Data First
Before you improve anything, make sure you trust the numbers. First, validate ideal cycle times with engineering. Then, walk the line and compare the counter to the reported count. Ideally, spend a couple of weeks building a baseline you believe in. Frankly, I would rather have an ugly honest 48 percent than a pretty fictional 72.
Step 2: Build a Loss Tree, Not Just a Score
Next, break the lost time into the Six Big Losses and then into specific reasons. For instance, “Availability 86.7 percent” is not actionable. By contrast, “capper jams cost 35 minutes per shift on average, mostly on the 500 ml format” is actionable. In my view, a simple Pareto chart of lost minutes by reason is the most useful single chart in any CI office.
Step 3: Attack the Biggest Bar, One at a Time
Then, pick the top loss and assign a small cross functional team: an operator, a maintenance tech, and a process engineer. Afterward, use structured problem solving such as A3 or 5 Why to get to root cause, rather than just a fix. Above all, resist the urge to launch ten projects at once. One finished project beats ten half done ones every single time.
Step 4: Match the Tool to the Loss
Different losses, of course, respond to different methods:
- Equipment failure responds to the same methods used to cut unplanned downtime: autonomous maintenance, preventive and predictive maintenance, and root cause analysis on repeat failures.
- Setup losses respond to SMED, one of the classic kaizen examples. For example, I have seen changeovers drop from 90 minutes to under 30 by separating internal and external tasks and staging tools properly.
- Small stops respond to operator led problem solving and basic equipment care, such as cleaning, tightening, and adjusting sensors and guides.
- Reduced speed responds to a hard look at why the line was slowed down in the first place. Quite often, the original problem was fixed years ago.
- Quality losses respond to error proofing, standard work, and tighter process control during startup.
Step 5: Make OEE Visible at the Line
In addition, put the live or shift level OEE on a board right where operators can see it, along with the top three losses from the last shift. Once the people running the machine can see the losses, they start fixing things you never would have noticed from an office.
Step 6: Hold the Gains
Lastly, every improvement should end in updated standard work, a revised PM schedule, or a changeover checklist. Otherwise, if the fix lives only in one technician’s head, it will be gone in six months.
Manual Versus Automated OEE Tracking
You do not need expensive software to start your first OEE calculation. In fact, some of the most productive OEE programs I have run began with a whiteboard, a paper downtime log, and a spreadsheet. Moreover, the discipline of writing down every stop teaches the team more about their equipment than any dashboard.
That said, once you are serious about Performance losses, manual tracking hits a wall. Simply put, people cannot log a 40 second stop every few minutes and still run the machine. At that point, a simple sensor on the infeed and outfeed and an automated counting system pays for itself quickly, mostly by exposing losses you did not know you had.
So, my rule of thumb is this: start manual to build the habit and the understanding, then automate to get the resolution.
Final Thoughts
After many years of doing this, I have come to believe that OEE calculation is one of the most honest conversations a plant can have with itself. It does not care about excuses or how busy everyone looked. Rather, it just asks how much good product came out compared to what was possible.
Therefore, if you take one thing from this article, let it be this: the number is the beginning, not the end. First, calculate it carefully. Then, break it into losses, go stand at the machine, and fix the biggest problem first. If you do that consistently, month after month, the OEE score will take care of itself.
Frequently Asked Questions
What is the basic formula for OEE calculation?
OEE equals Availability multiplied by Performance multiplied by Quality. Alternatively, you can calculate it directly as Good Count multiplied by Ideal Cycle Time, divided by Planned Production Time. For a detailed breakdown of both methods, see Vorne’s formula guide.
What is considered a world class OEE score?
85 percent is the commonly cited world class benchmark for discrete manufacturing, based on 90 percent Availability, 95 percent Performance, and 99.9 percent Quality. However, most plants operate closer to 60 percent. Read more in Vorne’s benchmark article.
What are the Six Big Losses in OEE?
They are equipment failure, setup and adjustments, small stops, reduced speed, production rejects, and startup rejects. In addition, each one maps to Availability, Performance, or Quality. Fabrico’s loss guide covers each one in depth.
Can Performance be higher than 100 percent?
No. If your Performance comes out above 100 percent, then your ideal cycle time is set too slow. Instead, use the design speed or best demonstrated rate. Evocon explains this in detail.
Should changeovers count against OEE?
Yes. Changeovers are a setup loss and therefore belong in Availability. Excluding them hides one of the most improvable losses on most lines. See eMaint’s maintenance guide.
What is the difference between OEE and TEEP?
OEE measures effectiveness during planned production time only. By contrast, TEEP (Total Effective Equipment Performance) measures against all calendar time, so it also captures time the equipment was not scheduled at all. The Vorne glossary explains both.
How often should I calculate OEE?
Ideally, calculate it every shift at the line level so operators can react, and then review weekly and monthly trends for improvement planning. Factbird’s quick guide offers a good overview of practical tracking.
References
- Vorne Industries. “OEE Calculation: Definitions, Formulas, and Examples.” OEE.com
- Vorne Industries. “World Class OEE: Set Targets to Drive Improvement.” OEE.com
- Vorne Industries. “OEE Glossary: Terms and Definitions.” OEE.com
- Wikipedia. “Overall Equipment Effectiveness.”
- eMaint. “OEE Calculation: Meaning, Formula, and Examples.”
- Evocon. “OEE Calculation: Formulas, Examples, and Insights.”
- Fabrico. “The 6 Big Losses of OEE.”
- Fabrico. “OEE Benchmarks: From Average 60% to World Class 85%.”
- Godlan. “The Six Big Losses in OEE: 2026 Manufacturing Data, Costs, and Benchmarks.”
- iFactory. “Six Big Losses in Manufacturing: The OEE Loss Taxonomy Explained.”
- Factbird. “A Quick Guide to OEE.”
- Nakajima, Seiichi. Introduction to TPM: Total Productive Maintenance. Productivity Press, 1988.