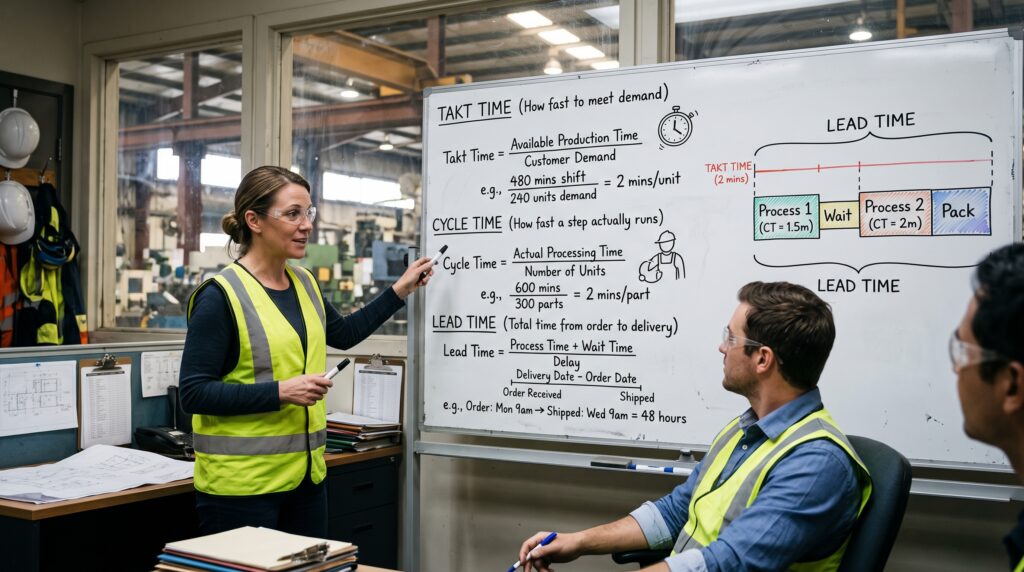
Understanding takt time helps manufacturers match production speed with customer demand and improve workflow efficiency.
The first time I balanced a line on my own, I got it wrong in a way I still think about. I had a stopwatch, a clipboard full of observations, and a supervisor who wanted to know why his welding cell kept falling behind. At first, I told him his cycle time was fine. In fact, it was, by itself. However, I had not held that number up against takt time, and when I finally did, the problem was obvious. His slowest station was taking longer than the customer’s beat allowed. As a result, he never had a chance.
Why Takt Time, Cycle Time, and Lead Time Get Confused
I have been an industrial engineer long enough to know that this mix up is not rare. In many plants, takt time, cycle time, and lead time get used interchangeably in production meetings, on whiteboards, and in vendor slide decks. Still, they are not the same thing. Instead, each one answers a different question. Consequently, if you swap them, you end up making decisions about staffing, capacity, and delivery promises based on the wrong number.
For that reason, this article walks through all three, gives you the formulas, and then works through real numbers. To keep it practical, I use a fabrication cell example built from the kind of shops I spend most of my time in. By the end, you should be able to calculate each metric, explain how they relate, and spot the mistakes that cost plants money.
Takt Time in Short: The Quick Version Before the Math
If you only remember one paragraph, make it this one.
Takt time is the pace the customer demands. In other words, it tells you how often you need to finish one unit.
Cycle time is the pace your process actually runs. Put simply, it tells you how often you do finish one unit, or how long one step takes.
Lead time is how long the customer waits. Specifically, it covers everything from the moment an order arrives until the product is in their hands, including all the waiting nobody likes to talk about.
To sum up, takt is a target, cycle time is a measurement, and lead time is an experience. Once you keep those three words in your head, most of the confusion goes away.
Takt Time: The Customer’s Heartbeat
Where the term takt time comes from
Takt is a German word for a beat or a precise interval, much like a conductor keeping an orchestra in time. According to the Lean Enterprise Institute, it was originally the interval at which aircraft were moved ahead to the next production station. Later, the concept became a cornerstone of the Toyota Production System and the broader set of lean manufacturing principles plant managers rely on today.
The takt time formula
Takt Time = Net Available Production Time ÷ Customer Demand (for the same period)
That is the entire formula. For example, the Lean Enterprise Institute uses a factory running 480 minutes per day against demand of 240 widgets, which gives a takt time of two minutes.
Getting the takt time inputs right
Although the formula is simple, the inputs are where people get into trouble.
First, net available time is the time your people or equipment are scheduled to work, minus planned breaks, lunch, startup meetings, and planned cleaning. However, it does not subtract unplanned downtime, breakdowns, or changeovers. After all, those are losses your process has to absorb. Therefore, hiding them inside the takt calculation makes the target look easier than it really is.
Second, customer demand is the quantity the customer actually needs in that same period. In other words, it is not what the sales team hopes for, not the forecast from two quarters ago, and not the number the plant manager wants to build to keep machines busy. Instead, use real demand, leveled over a sensible period.
Worked example 1: Takt time for a bracket welding cell
To start, picture a mid sized fabrication shop making steel mounting brackets for an equipment OEM. The shop runs one shift, five days a week.
- Shift length: 8.5 hours = 510 minutes
- Lunch: 30 minutes
- Two breaks at 10 minutes each: 20 minutes
- Daily startup and safety huddle: 10 minutes
Net available time = 510 minus 30 minus 20 minus 10 = 450 minutes per day
Next, convert to seconds, because takt for repetitive work is usually expressed in seconds: 450 × 60 = 27,000 seconds
Meanwhile, the customer orders 1,800 brackets per week. Spread across five days, that comes to 360 brackets per day.
Takt Time = 27,000 ÷ 360 = 75 seconds per bracket
In practice, this means a finished bracket needs to come off the end of that cell every 75 seconds. If you go faster than that, you are building inventory nobody asked for. On the other hand, if you go slower, you fall behind, which eventually means overtime, expediting, or a late shipment.
Takt time moves when demand moves
This next part surprises people. Takt time is not a property of your equipment. As a result, you cannot improve it with a kaizen event. Instead, it changes only when the available time or the demand changes.
For instance, say the OEM wins a new contract and bumps the order to 2,250 brackets per week, or 450 per day.
New Takt Time = 27,000 ÷ 450 = 60 seconds per bracket
Notice that the machines, people, and shift stayed the same. Even so, the beat just got 15 seconds faster. Similarly, Art Byrne makes the same point at the Lean Enterprise Institute: when demand doubles and available time holds steady, takt is cut in half. Ultimately, your process either keeps up or it does not, and that is exactly what cycle time tells you.
Cycle Time: How Your Process Compares to Takt Time
Two common definitions, both valid
Here I have to be honest about the terminology. On the shop floor, “cycle time” gets used two ways, so you need to know which one someone means.
On one hand, operation cycle time is how long a single step takes to complete one unit. Typically, you measure it with a stopwatch at the station, from the moment the operator starts the bracket until they start the next one.
On the other hand, process cycle time (sometimes called output interval) is how often units actually exit the whole process. The common formula is:
Cycle Time = Net Production Time ÷ Number of Units Produced
Both matter, because they serve different purposes. Operation cycle times tell you where the bottleneck is. Meanwhile, process cycle time tells you whether the system as a whole is keeping pace with takt.
Worked example 2: Measuring cycle times against takt time
Now let us go back to the bracket cell, which has four stations. First, I timed each one over ten consecutive cycles. Then I took the median. Here are the results:
| Station | Median Cycle Time |
|---|---|
| 1. Saw cut and deburr | 52 seconds |
| 2. Weld | 88 seconds |
| 3. Grind and finish | 61 seconds |
| 4. Inspect and pack | 40 seconds |
| Total work content | 241 seconds |
Next, compare each station against the 75 second takt time.
As you can see, cut, grind, and inspect are all under 75. However, weld is at 88 seconds. In other words, that station is 13 seconds over takt on every single bracket. Consequently, when you multiply that across a day, the cell simply cannot hit 360 units, no matter how hard anyone works.
The comparison that matters most
This is the comparison I failed to make on my first job. A station can look busy and productive, and the operator can be doing excellent work. Even so, the station can still be the reason the whole cell is late.
Why I use the median, not the average
For example, here are the actual ten weld readings in seconds:
84, 86, 88, 91, 87, 85, 112, 88, 86, 89
The average is 89.6 seconds, whereas the median is 87.5 seconds. That 112 second reading was a wire spool change. Of course, it is real, and it needs its own countermeasure, ideally found through proper root cause analysis. Still, it is not the repeatable cycle. So, if you average it in, you blur two different problems together. For that reason, I record the median as the cycle time and log the outliers separately as losses to attack, the same way you would track them in an OEE calculation.
Worked example 3: Process cycle time from output
At the end of one day, the cell shipped 300 brackets in its 450 available minutes.
Process Cycle Time = 27,000 ÷ 300 = 90 seconds per bracket
Not surprisingly, that lines up with the weld station. After all, the whole cell can only go as fast as its slowest step, plus some losses. Therefore, the gap against takt is clear:
- Required: 360 per day at 75 seconds
- Actual: 300 per day at 90 seconds
- Shortfall: 60 brackets per day, or 300 per week
Above all, that is a number a plant manager understands.
Using takt time and cycle time to size the crew
Once you have total work content and takt time, you can also estimate the minimum number of operators:
Minimum Operators = Total Work Content ÷ Takt Time
So, 241 ÷ 75 = 3.21, which rounds up to 4 operators
Likewise, at the higher demand scenario with a 60 second takt:
241 ÷ 60 = 4.02, which rounds to 5 operators. Alternatively, you find two seconds of waste and do it with four. Personally, I always push for the second option first. After all, rounding up to a fifth person to cover 0.02 of a workload is expensive. Besides, two seconds of waste is almost always sitting in plain view.
Fixing a bottleneck that misses takt time
Even with four operators and a 75 second takt, the weld station still has to come below 75. Here are a few options I would put on the table:
- Split the work. For example, separate tack welding (about 44 seconds) from final welding (about 44 seconds). As a result, you get two shorter stations, both well under takt.
- Offload to a neighbor. Since grind is at 61 seconds, it has 14 seconds of room. Therefore, some weld cleanup could shift there.
- Attack the method. In addition, better fixturing, a quicker clamp, or pre positioned wire can cut seconds off every cycle. A disciplined 5S methodology at the station often surfaces these quickly.
Leave a buffer below takt time
Furthermore, I do not balance stations right up to 75 seconds. Instead, I aim for a planned cycle time around 85 to 90 percent of takt, which is roughly 64 to 68 seconds here. That way, the buffer absorbs normal variation, minor stops, and the occasional quality check without the line falling behind. Admittedly, balancing to 100 percent of takt looks efficient on paper. In reality, though, it falls apart by ten in the morning.
Lead Time: What the Customer Feels
The lead time formula
The most common way to write it is:
Lead Time = Preprocessing Time + Processing Time + Postprocessing Time
To break that down, preprocessing covers order entry, planning, scheduling, and waiting for material. Next, processing is the actual work, which includes the cycle times we just measured. Finally, postprocessing covers inspection holds, finished goods storage, staging, and shipping.
Alternatively, there is the version I use more often when mapping a value stream:
Lead Time = Sum of All Processing Times + Sum of All Queue and Wait Times
Worked example 4: Lead time for one bracket order
Now let us follow a single order through the plant.
| Step | Time |
|---|---|
| Order entry and scheduling | 1 day |
| Waiting for steel bar stock | 3 days |
| Queue before welding | 1.5 days |
| Outsourced powder coat, including transport both ways | 4 days |
| Finished goods storage before shipping | 2 days |
| Total wait time | 11.5 days |
| Total processing (cut, weld, grind, inspect) | 241 seconds, about 4 minutes |
Lead Time ≈ 11.5 days
Now look at those two numbers next to each other. On one side, there are four minutes of touch time. On the other, there are eleven and a half days of waiting.
How much of lead time adds value
To put that in perspective, we can express it as a ratio using the plant’s working time (11.5 days × 27,000 seconds = 310,500 seconds). The share of lead time that is actual value adding work is:
241 ÷ 310,500 = 0.08 percent
Unfortunately, that figure is not unusual. In fact, I have mapped plenty of value streams where the number came in below one percent. More importantly, it explains something critical: you can cut your cycle time in half and barely move your lead time. For example, if the weld station drops from 88 to 44 seconds, the customer still waits about 11.5 days. That is because the time is hiding in the queues, not at the machines.
Worked example 5: Lead time with Little’s Law
When you cannot follow a single order through, Little’s Law gets you an estimate from data you probably already have. Notably, it was proven by MIT professor John Little in 1961, and it holds for any stable flow system over a long enough period.
Lead Time = Work in Process ÷ Throughput
For instance, say a physical count shows 2,400 brackets sitting somewhere in the system. That includes raw stock cut to length, parts waiting at weld, parts out at the coater, and finished goods. Meanwhile, the cell ships 360 per day.
Lead Time = 2,400 ÷ 360 = 6.7 days
Now suppose the team caps WIP using kanban and holds the total to 1,080 brackets, while throughput stays the same.
Lead Time = 1,080 ÷ 360 = 3 days
In this case, nobody worked faster, and nobody bought a new machine. Instead, the plant simply stopped letting inventory pile up between steps. As a result, the customer’s wait dropped by more than half.
A caution about cutting WIP
That said, here is one caution from experience: do not cut WIP so far that you starve the bottleneck. If the weld station runs dry, throughput falls. Then, by the same equation, lead time goes right back up. So, reduce WIP in steps and watch what happens at the constraint. Automakers learned this lesson the hard way when lean buffers met real disruption, as covered in these just-in-time inventory failures.
How Takt Time, Cycle Time, and Lead Time Fit Together
To make this easier, here is a side by side summary I hand to new supervisors:
| Takt Time | Cycle Time | Lead Time | |
|---|---|---|---|
| Question it answers | How fast must we produce? | How fast do we produce? | How long does the customer wait? |
| Set by | Customer demand | Process, people, equipment | The whole system, especially queues |
| Formula | Available time ÷ demand | Production time ÷ units produced | Pre + processing + post time, or WIP ÷ throughput |
| Typical unit | Seconds or minutes | Seconds or minutes | Hours, days, or weeks |
| Can you improve it directly? | No | Yes | Yes |
| Main use | Line balancing, staffing | Finding bottlenecks | Delivery promises, flow |
The relationships worth remembering
First, cycle time should sit just under takt time. If it is higher, you cannot meet demand. Conversely, if it is far lower, you are probably overstaffed or overproducing.
Second, lead time is always longer than cycle time, often by orders of magnitude, because it includes waiting.
Finally, takt time drives everything else. Not only does it set the target your cycle times must hit, but it also tells you how much WIP and lead time you can tolerate before the customer notices.
Takt Time Outside the Assembly Line
Of course, industrial services work is not always a moving line of identical brackets. In fact, plenty of my work has been in maintenance shops, rebuild centers, and job shops where every order looks a little different. Even so, takt time still works. You just widen the window.
Worked example 6: Takt time for a pump rebuild shop
For example, a maintenance contractor rebuilds industrial centrifugal pumps for refineries and water treatment plants. The shop runs one shift with 450 net minutes per day, five days a week, so it has 2,250 minutes per week. On average, customers send in six rebuilds per week.
Takt Time = 2,250 ÷ 6 = 375 minutes per pump
In other words, that is about six and a quarter hours. So, on average, every pump has to clear the shop at that pace. However, if the teardown, inspection, machining, reassembly, and test sequence takes eight hours of bench time at its slowest stage, the shop is structurally behind before the week even starts.
Treat takt time as an average in service work
In service and repair settings, therefore, I treat takt as an average pace over a day or a week, not a strict second by second rhythm. Naturally, work content varies, and that is fine. Similarly, Velaction points out that because customer driven processes carry so much variation, service and office work is much harder to tie to a precise pace. For that reason, takt works best there as an average. Ultimately, the discipline of knowing the number is what matters.
Common Takt Time Mistakes I See in Plants
Mistakes with the takt time calculation
1. Using total shift time instead of net available time. For example, if you forget to subtract breaks and lunch, your takt looks longer than it really is. As a result, you understaff the cell.
2. Subtracting unplanned downtime from available time. In effect, this bakes your losses into the target. Instead, takt should reflect the time you planned to work, because downtime is a problem to solve, not an allowance.
3. Calculating takt once and forgetting it. After all, demand shifts every quarter, and sometimes every month. Therefore, I recalculate takt whenever the customer schedule changes meaningfully and feed it back into production scheduling. Then I post it at the cell so everyone knows the current beat.
Mistakes with cycle time and lead time
4. Reporting cycle time without the takt target next to it. On its own, “our weld cycle is 88 seconds” means nothing. However, against a 75 second takt, it means the cell is losing 60 brackets a day.
5. Balancing stations to exactly 100 percent of takt. Simply put, real processes vary. So, leave yourself a buffer.
6. Trying to fix lead time by speeding up machines. If 99.9 percent of lead time is waiting, faster machines will not help. Instead, shrink the queues.
7. Averaging cycle times that include outliers. Rather than averaging, use the median for the repeatable cycle and track the outliers as separate losses.
A Practical Takt Time Routine You Can Start Tomorrow
If you want to put this into practice on your own floor, here is the sequence I follow on almost every engagement:
- First, get the real customer demand for the next period from the actual schedule, not a forecast summary.
- Next, calculate net available time with the supervisor, line by line, and agree on it.
- Then calculate takt time and post it visibly at the cell.
- After that, time every station for at least ten cycles, record the median, and list the outliers.
- Also, build a simple bar chart of station cycle times with a horizontal line at takt, so the bottleneck jumps off the page.
- In addition, count WIP and divide by daily throughput to estimate lead time.
- Similarly, walk one order from receipt to shipment and write down every wait, then compare that to step 6.
- Finally, fix the bottleneck first, and then attack the biggest queue.
Honestly, that routine has saved more overtime budgets than any software tool I have ever been asked to evaluate.
Final Thoughts on Takt Time
Three views of the same system
Takt time, cycle time, and lead time are not competing metrics. Rather, they are three views of the same system. Takt time tells you what the customer needs. Meanwhile, cycle time tells you whether your process can deliver it. Finally, lead time tells you how the customer experiences your entire operation, including the parts nobody is actively working on.
Discipline beats complexity
So, get the definitions straight, calculate them with honest inputs, and keep them side by side. Looking back, the supervisor who asked me why his cell kept falling behind did not need a new welder or a second shift. Instead, he needed a takt time posted at the end of his line and a weld station that could hit it. Once we split that station, his cell made rate within a week.
In the end, the math is simple. However, the discipline of using it every day is what separates plants that hit their numbers from plants that explain why they missed them.
Frequently Asked Questions About Takt Time
What is takt time in simple terms?
Simply put, takt time is the rate at which you need to finish one unit to keep up with customer demand. To calculate it, divide your net available working time by the number of units customers need in that period. For the standard definition, see the Lean Enterprise Institute lexicon entry on takt time.
What is the difference between takt time and cycle time?
Takt time is a target set by customer demand. In contrast, cycle time is a measurement of how fast your process actually produces. So, if cycle time is higher than takt time, you cannot meet demand. For more detail, iSixSigma covers this in its article on takt time vs cycle time.
Should cycle time be lower than takt time?
Yes, slightly. Generally, engineers aim for a planned cycle time around 85 to 90 percent of takt to absorb normal variation. However, if cycle time is far below takt, you may be overstaffed or overproducing. Velaction’s guide to takt time basics explains why both extremes cause problems.
Is lead time the same as cycle time?
No. Cycle time covers processing only, whereas lead time covers the full span from order to delivery, including queues, transport, and storage. As a result, lead time is almost always much longer. SoftwareConnect breaks this down in takt vs cycle vs lead time.
How do you calculate lead time using Little’s Law?
Divide your total work in process by your throughput rate. For example, 2,400 units of WIP and a throughput of 360 units per day gives a lead time of about 6.7 days. Fabrico walks through this in its explanation of Little’s Law in manufacturing.
Can you improve takt time?
Not directly. That is because takt time changes only when customer demand or available working time changes. Instead, what you can improve is cycle time, so your process keeps pace with takt. Art Byrne discusses this in why takt time matters in a lean turnaround.
Does takt time apply outside manufacturing?
Yes. In fact, repair shops, maintenance contractors, order processing, and other service operations can all use takt time, usually as an average pace over a day or week. For example, Rutgers Executive Education shows a service case in its piece on takt time and customer demand.
References
- Lean Enterprise Institute. Takt Time: Lean Lexicon Definition
- Byrne, A. Lean Enterprise Institute. Ask Art: Why Is Takt Time So Important in a Lean Turnaround?
- iSixSigma. Takt Time vs. Cycle Time: When Do You Choose What to Use?
- SoftwareConnect. Takt Time vs. Cycle Time vs. Lead Time: The Differences Explained
- Six Sigma Development Solutions. Takt Time vs Cycle Time vs Lead Time
- Velaction. Takt Time: Definition, Calculation, and Lean Office Application
- Simplilearn. Time Confusion: Cycle Time vs Takt Time vs Lead Time
- GoLeanSixSigma. Takt Time Definition
- Fabrico. Little’s Law in Manufacturing: WIP, Throughput, Lead Time
- HackerNoon. Your Team Isn’t the Problem, But Your WIP Is
- Rutgers Executive Education. Lean Six Sigma: Takt Time to Meet Customer Demand
- UMass Amherst Bootcamps. Takt Time vs Cycle Time vs Lead Time


